Ultrasonic-Coated Anodes for Trivalent Chromium Plating
Trivalent chromium plating is used for decorative and functional surface finishing, but achieving a consistent deposit across complex components can be challenging. Recesses, deep features and changing part geometry create local differences in current density. Bath chemistry, anode condition and cell configuration all affect throwing power, appearance and coating thickness. Unstable anode behaviour can add another source of process variation.
Ultrasonic spray coating offers a controlled manufacturing method for applying catalytic layers to dimensionally stable anodes used in trivalent chromium systems. When the substrate geometry and catalyst composition are designed for the bath, a consistent active surface can support repeatable current distribution and reliable finishing. The process must be validated against the specific trivalent chromium chemistry, since proprietary bath formulations can differ significantly.
Technology Principle: Why Ultrasonic Spray Coating?
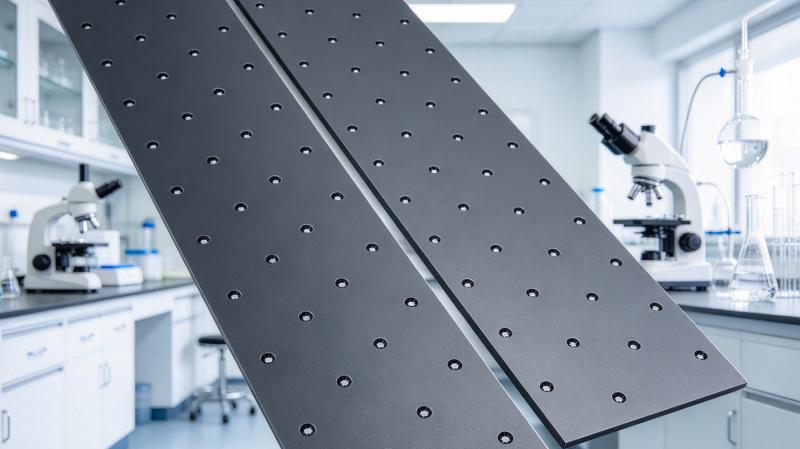
An anode in a trivalent chromium plating cell supports the anodic reactions that maintain the electrochemical balance of the bath. The electrode must remain compatible with the electrolyte and should not introduce unwanted contamination or destabilize bath chemistry. A dimensionally stable anode uses a corrosion-resistant substrate with a catalytic coating. The coating composition, active area and spacing are selected to suit the operating current and bath formulation.
Ultrasonic coating deposits catalyst precursor as fine droplets on the prepared substrate. Controlled overlap and liquid feed help create an even layer, which is then dried and thermally converted as required by the chemistry. The final anode is assessed for coating integrity, dimensional accuracy and electrochemical response in the actual plating bath.
Product Structure and Key Components
Manufacturing equipment includes an ultrasonic generator and nozzle, metered precursor delivery, a programmable motion system, substrate fixtures, drying and thermal treatment, and inspection. Because finishing anodes may have bars, plates or custom shapes, the fixture must preserve the required geometry and ensure coverage of edges and recessed features. Electrical contact areas may need masking or a separate finishing specification.
Core Advantages for Industrial Electrode Manufacturing
- Dimensional stability: a fixed anode geometry helps maintain consistent spacing from the workpiece.
- Uniform active surface: controlled coating coverage can reduce local differences in anodic behaviour.
- Improved process consistency: stable anode performance supports repeatable finishing recipes.
- Longer service planning: durable catalyst layers can reduce maintenance frequency when bath conditions are controlled.
- Complex-part support: anode placement and shielding can be engineered for recesses and decorative surfaces.
Typical Applications and Process Validation
Potential applications include decorative chromium finishes, functional components and parts with complex geometries where throwing power is important. The anode is only one part of the solution. Rack design, auxiliary anodes, shields, agitation, current waveform, bath temperature and proprietary additive package may be equally important. Trial plating should include representative components and thickness mapping at both exposed and recessed locations.
How to Evaluate the Process Before Choosing Equipment
A useful evaluation begins with the electrolyte, substrate, operating current density, temperature, flow pattern and required service life. Record the current anode geometry and coating condition, then define the performance problem in measurable terms: deposit-thickness variation, cell voltage, coating consumption, bath contamination, maintenance frequency or rejected product. These measurements establish a baseline and prevent a new coating process from being judged only by appearance.
For a laboratory trial, use representative substrate coupons and the actual production electrolyte wherever practical. Keep substrate preparation, masking, coating loading and thermal treatment under documented control. Change one process variable at a time when establishing the initial window. A visually uniform coating is encouraging, but it does not by itself prove adhesion, electrochemical activity or long-term durability. Include electrochemical measurements and an operating test that reflects the intended duty cycle.
Equipment Architecture and Process Control
An ultrasonic coating system normally combines a liquid-delivery unit, ultrasonic atomizing nozzle, transducer and generator, motion platform, substrate fixture, extraction or drying provisions, and a control interface. The nozzle converts liquid into a fine, relatively low-velocity mist. The generator maintains the required vibration, while the liquid-delivery system controls feed stability. A motion system manages the relative path between the nozzle and substrate so that overlapping passes create a consistent deposited layer.
Important design decisions include wetted-part compatibility, nozzle material, liquid-path cleanability, fixture rigidity, motion repeatability and the ability to monitor flow and ultrasonic power. Corrosion-resistant materials should be selected against the actual precursor chemistry rather than chosen by appearance alone. Where a process uses flammable solvents, the complete installation, ventilation, electrical equipment and operating procedures must be assessed for the applicable hazardous-area requirements. Do not assume that an individual component’s rating certifies the complete line.
Key Process Variables and Performance Indicators
There is no universal power, flow-rate, traverse-speed or coating-thickness setting for every catalyst formulation. The correct operating window depends on viscosity, surface tension, solids loading, solvent volatility, particle size, substrate temperature, nozzle-to-surface distance and the desired loading. Establish a stable window through trials and document the formulation and environmental conditions alongside every result.
Track coating mass per unit area, thickness distribution, edge-to-centre variation, adhesion, surface morphology, electrical contact resistance where relevant, electrochemical activity and durability under representative cycling. At production scale, also monitor line speed, uptime, material utilization, cleaning interval and batch-to-batch variation. Compare these indicators with the existing process using the same sampling plan. This creates a defensible basis for calculating yield, operating cost and return on investment.
Practical Limitations and Troubleshooting
Ultrasonic atomization can improve control, but it cannot compensate for an unstable precursor, contaminated substrate or poorly designed cell. High viscosity, rapid solvent evaporation, agglomerated solids or a formulation outside the nozzle’s workable range may cause unstable atomization or irregular deposition. Poor wetting can create pinholes or dewetting; excessive local loading can cause cracking during drying or thermal treatment; insufficient surface preparation can cause weak adhesion.
When defects appear, first verify substrate cleanliness and surface condition, then check liquid homogeneity, feed stability, nozzle condition, ambient airflow, substrate temperature and motion overlap. Confirm that the drying and thermal-treatment profile is compatible with the catalyst chemistry and substrate. Avoid changing several variables simultaneously, because that makes root-cause analysis difficult. For corrosive or hazardous electrolytes, use appropriate containment, ventilation, personal protective equipment and waste-handling procedures.
From Laboratory Trials to Production
Small-scale equipment is useful for screening formulations, confirming wetting behaviour and comparing catalyst loading. A pilot platform should reproduce the important production variables, including nozzle motion, substrate handling, drying conditions and repeatable liquid delivery. A production line adds throughput, automation, process monitoring, maintenance access and documented quality controls. Scaling should preserve the deposition mechanism rather than simply increasing liquid flow or ultrasonic power.
Before specifying a system, prepare a sample set that includes the real substrate, catalyst precursor and target coating loading. Agree on acceptance criteria before the trial, and retain reference samples for later comparison. The final specification should identify the process window, inspection method, maintenance interval, changeover procedure and the responsibilities for precursor preparation and quality release.
Selection Guidance and Next Steps
Choose equipment around the substrate dimensions, required throughput, chemistry, coating area, target loading and degree of automation. Confirm whether the application needs a single nozzle, multiple nozzles, a translating stage, a roll-to-roll arrangement or a custom fixture. Ask how the system controls liquid delivery, monitors ultrasonic operation, records recipes and supports cleaning. A pilot trial is particularly valuable when the catalyst formulation or electrolyte is new.
Cheersonic can discuss application requirements, coating trials, process development and customized ultrasonic coating equipment. Qualified manufacturers and R&D teams are invited to share substrate samples, precursor information and target performance criteria so that a practical test plan can be agreed.
Explore Cheersonic ultrasonic coating equipment solutions or contact market2@cheersonic.com to discuss a catalyst-coating project and arrange a coating sample test.