Ultrasonic Spray-Coated MMO Titanium Anodes for Electrogalvanizing Steel Lines
Continuous electrogalvanizing lines must deposit a controlled zinc layer on moving steel strip while maintaining high throughput and consistent surface quality. Anode degradation, uneven current distribution and maintenance stoppages can affect coating weight, line stability and production cost. Because a continuous line operates under demanding electrical and mechanical conditions, the anode system must be reliable, dimensionally stable and compatible with the electrolyte.
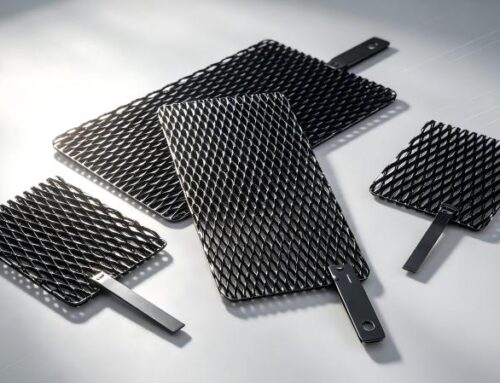
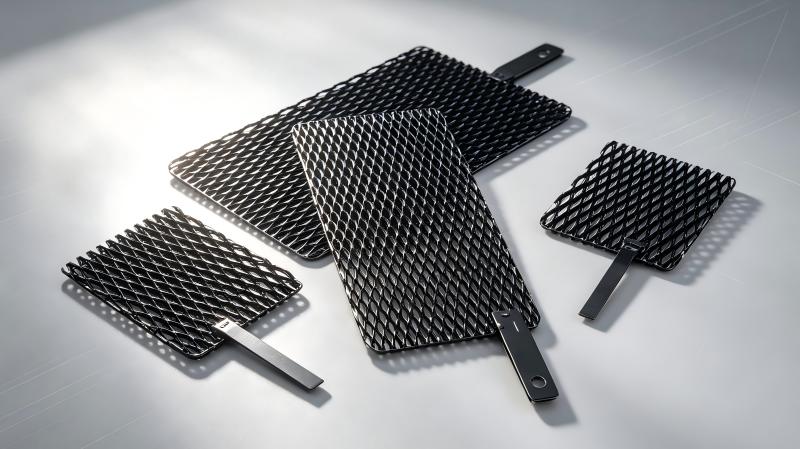
Ultrasonic spray coating is a controlled manufacturing method for applying mixed-metal-oxide catalytic layers to titanium substrates. A properly designed MMO titanium anode can provide a stable insoluble electrode surface for electrogalvanizing applications. Its value lies in supporting controlled current delivery, planned maintenance and reduced dependence on soluble anode consumption, subject to validation in the specific line configuration.
Technology Principle: Why Ultrasonic Spray Coating?
The titanium substrate provides a mechanically robust, conductive base, while the MMO coating provides the catalytic surface required for the anodic reaction in the selected electrolyte. Ultrasonic atomization deposits a precursor solution in controlled passes. Drying and thermal conversion create the oxide coating. Composition, loading and heat-treatment conditions must be engineered for the electrolyte and operating potential; there is no universal MMO recipe for every steel-plating line.
Compared with coarse pressure spraying or manual application, ultrasonic deposition can offer finer control over liquid delivery and layer build-up. The process still depends on correct titanium preparation, precursor chemistry and thermal treatment. These factors govern adhesion and durability as much as the atomizing method itself.
Product Structure and Key Components
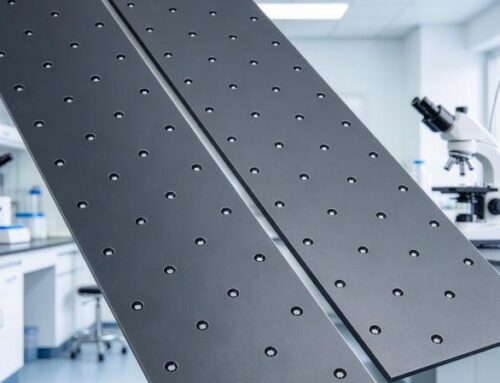
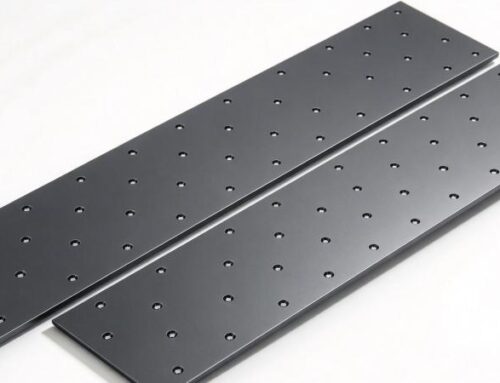
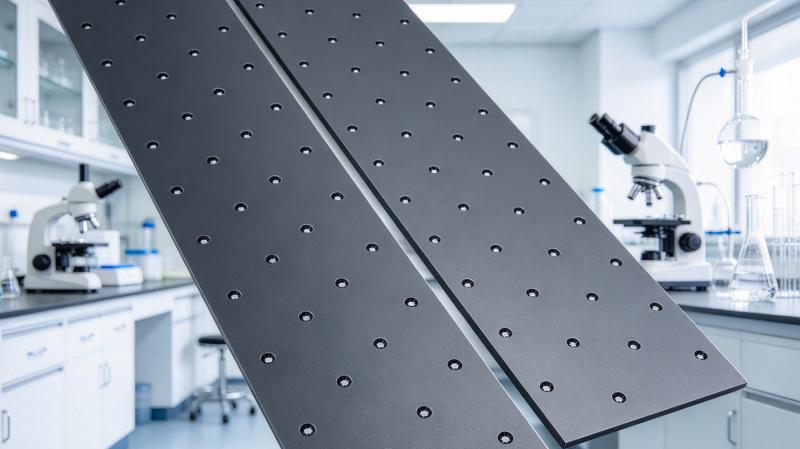
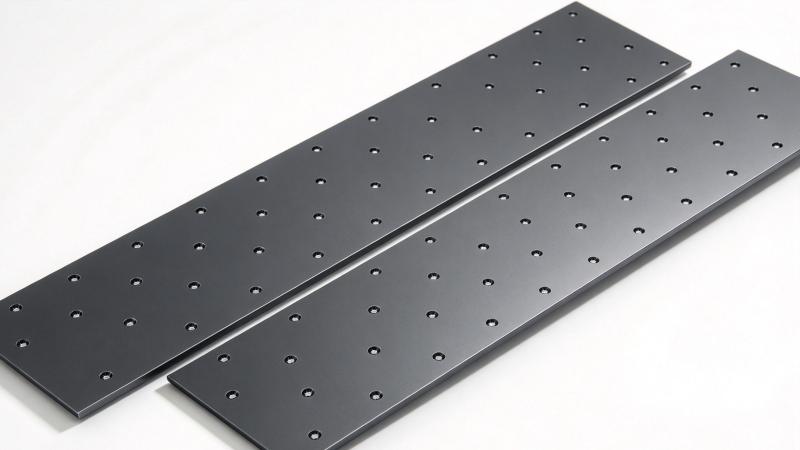
Coating equipment can be configured for flat plates, shaped anodes or elongated components used in vertical, horizontal, gravity-fed or radial electrogalvanizing cells. The system includes liquid preparation and delivery, ultrasonic nozzle and generator, a precision motion stage, fixtures, drying and thermal treatment, and quality inspection. Long anodes may require multi-zone motion control to maintain consistent coverage along their full length.
Core Advantages for Industrial Electrode Manufacturing
- Current-distribution control: consistent active coating and accurate geometry help support uniform anodic behaviour.
- Long service potential: application-matched MMO chemistry can provide durable operation when correctly maintained.
- Refurbishment options: suitable titanium substrates may be candidates for inspection and recoating, subject to condition assessment.
- Reduced unplanned maintenance: predictable coating performance supports planned service intervals.
- Process control: insoluble anodes can help stabilize electrode geometry and reduce zinc losses associated with uncontrolled anode dissolution.
Typical Applications and Process Validation
Potential configurations include vertical, horizontal, gravity and radial electrogalvanizing cells. Each has different flow, strip path, anode-to-strip distance and mechanical constraints. The coating design must account for electrolyte composition, current density, line speed, temperature and the required zinc coating weight. A production trial should examine coating uniformity across strip width and along the line, as well as anode voltage and maintenance behaviour.
How to Evaluate the Process Before Choosing Equipment
A useful evaluation begins with the electrolyte, substrate, operating current density, temperature, flow pattern and required service life. Record the current anode geometry and coating condition, then define the performance problem in measurable terms: deposit-thickness variation, cell voltage, coating consumption, bath contamination, maintenance frequency or rejected product. These measurements establish a baseline and prevent a new coating process from being judged only by appearance.
For a laboratory trial, use representative substrate coupons and the actual production electrolyte wherever practical. Keep substrate preparation, masking, coating loading and thermal treatment under documented control. Change one process variable at a time when establishing the initial window. A visually uniform coating is encouraging, but it does not by itself prove adhesion, electrochemical activity or long-term durability. Include electrochemical measurements and an operating test that reflects the intended duty cycle.
Equipment Architecture and Process Control
An ultrasonic coating system normally combines a liquid-delivery unit, ultrasonic atomizing nozzle, transducer and generator, motion platform, substrate fixture, extraction or drying provisions, and a control interface. The nozzle converts liquid into a fine, relatively low-velocity mist. The generator maintains the required vibration, while the liquid-delivery system controls feed stability. A motion system manages the relative path between the nozzle and substrate so that overlapping passes create a consistent deposited layer.
Important design decisions include wetted-part compatibility, nozzle material, liquid-path cleanability, fixture rigidity, motion repeatability and the ability to monitor flow and ultrasonic power. Corrosion-resistant materials should be selected against the actual precursor chemistry rather than chosen by appearance alone. Where a process uses flammable solvents, the complete installation, ventilation, electrical equipment and operating procedures must be assessed for the applicable hazardous-area requirements. Do not assume that an individual component’s rating certifies the complete line.
Key Process Variables and Performance Indicators
There is no universal power, flow-rate, traverse-speed or coating-thickness setting for every catalyst formulation. The correct operating window depends on viscosity, surface tension, solids loading, solvent volatility, particle size, substrate temperature, nozzle-to-surface distance and the desired loading. Establish a stable window through trials and document the formulation and environmental conditions alongside every result.
Track coating mass per unit area, thickness distribution, edge-to-centre variation, adhesion, surface morphology, electrical contact resistance where relevant, electrochemical activity and durability under representative cycling. At production scale, also monitor line speed, uptime, material utilization, cleaning interval and batch-to-batch variation. Compare these indicators with the existing process using the same sampling plan. This creates a defensible basis for calculating yield, operating cost and return on investment.
Practical Limitations and Troubleshooting
Ultrasonic atomization can improve control, but it cannot compensate for an unstable precursor, contaminated substrate or poorly designed cell. High viscosity, rapid solvent evaporation, agglomerated solids or a formulation outside the nozzle’s workable range may cause unstable atomization or irregular deposition. Poor wetting can create pinholes or dewetting; excessive local loading can cause cracking during drying or thermal treatment; insufficient surface preparation can cause weak adhesion.
When defects appear, first verify substrate cleanliness and surface condition, then check liquid homogeneity, feed stability, nozzle condition, ambient airflow, substrate temperature and motion overlap. Confirm that the drying and thermal-treatment profile is compatible with the catalyst chemistry and substrate. Avoid changing several variables simultaneously, because that makes root-cause analysis difficult. For corrosive or hazardous electrolytes, use appropriate containment, ventilation, personal protective equipment and waste-handling procedures.
From Laboratory Trials to Production
Small-scale equipment is useful for screening formulations, confirming wetting behaviour and comparing catalyst loading. A pilot platform should reproduce the important production variables, including nozzle motion, substrate handling, drying conditions and repeatable liquid delivery. A production line adds throughput, automation, process monitoring, maintenance access and documented quality controls. Scaling should preserve the deposition mechanism rather than simply increasing liquid flow or ultrasonic power.
Before specifying a system, prepare a sample set that includes the real substrate, catalyst precursor and target coating loading. Agree on acceptance criteria before the trial, and retain reference samples for later comparison. The final specification should identify the process window, inspection method, maintenance interval, changeover procedure and the responsibilities for precursor preparation and quality release.
Selection Guidance and Next Steps
Choose equipment around the substrate dimensions, required throughput, chemistry, coating area, target loading and degree of automation. Confirm whether the application needs a single nozzle, multiple nozzles, a translating stage, a roll-to-roll arrangement or a custom fixture. Ask how the system controls liquid delivery, monitors ultrasonic operation, records recipes and supports cleaning. A pilot trial is particularly valuable when the catalyst formulation or electrolyte is new.
Cheersonic can discuss application requirements, coating trials, process development and customized ultrasonic coating equipment. Qualified manufacturers and R&D teams are invited to share substrate samples, precursor information and target performance criteria so that a practical test plan can be agreed.
Explore Cheersonic ultrasonic coating equipment solutions or contact market2@cheersonic.com to discuss a catalyst-coating project and arrange a coating sample test.